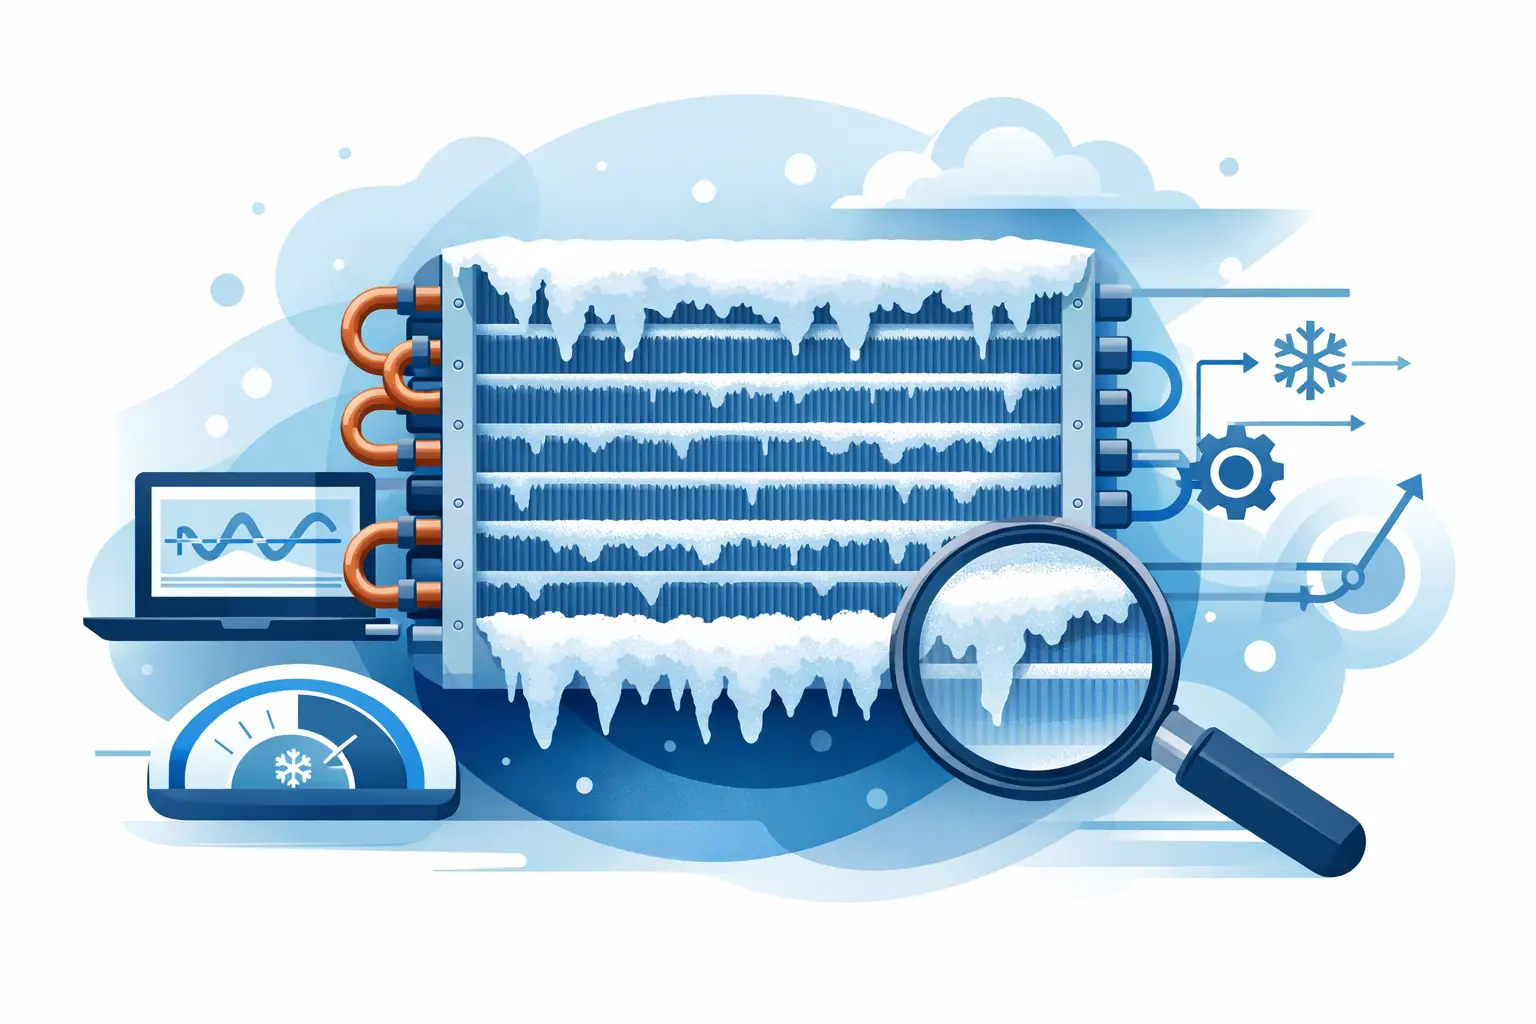
A coil that meets capacity at clean conditions can become unacceptable well before the refrigeration system reaches a conventional low-temperature limit. As frost accumulates, air passages contract, fan operating point shifts, air-side pressure drop rises, and the coil's effective heat transfer behavior changes continuously. To simulate evaporator frosting credibly, the model must treat frost as a transient, coupled thermal and airflow problem rather than a fixed capacity correction.
For DX evaporators, the result is especially sensitive to local refrigerant conditions. Circuiting, distributor behavior, tube-to-tube temperature variation, and air maldistribution can make frost growth nonuniform across the face area. A useful simulation therefore resolves the physical mechanisms that govern where frost begins, how it grows, and when the resulting loss of airflow or capacity requires defrost.
Why clean-coil calculations are not enough
A clean-coil selection establishes a starting point, not an operating limit. Once a surface temperature falls below the local air dew point and below freezing, water vapor can deposit as frost. That layer adds thermal resistance, reduces free flow area, modifies fin efficiency, and increases air-side pressure loss. These effects feed back into one another.
As the air side becomes more restrictive, the fan may deliver less air. Lower airflow changes the air-side heat transfer coefficient and may reduce the sensible and latent load presented to downstream coil sections. Meanwhile, changing refrigerant evaporation pressure can alter local tube-wall temperatures and redistribute capacity across the circuit. A model that applies a single overall fouling factor cannot represent these interactions with sufficient fidelity for design validation.
The design objective also matters. A low-temperature freezer evaporator may be governed by time between defrosts and fan power. A medium-temperature display case coil may be more sensitive to product-temperature stability, discharge-air distribution, and recoverability after defrost. Comfort-cooling coils can experience frost under abnormal airflow, low-load operation, or heat-pump heating conditions, where frost may be localized and strongly affected by outdoor air state.
Inputs required to simulate evaporator frosting
The model should begin with the same geometric and operating detail required for a credible clean-coil analysis. This includes fin pitch and thickness, tube outside diameter, row count, circuitry, face area, coil depth, air velocity distribution, refrigerant type, superheat control assumptions, and entering air dry-bulb temperature and humidity ratio.
Frosting analysis adds parameters that describe the deposited layer and the air-side system. Frost density, effective thermal conductivity, surface roughness, permeability, and porosity influence both heat transfer and pressure drop. These properties are not constant in practice. Newly formed frost is typically porous and low density; as exposure time increases, compaction, sintering, local melting, and refreezing can change its structure.
Fan behavior must also be represented with more care than a fixed airflow input. The coil pressure-drop increase moves the operating point along the fan curve. If the equipment has electronically commutated fan control, variable-speed control logic may partially offset that shift. If it has a fixed-speed fan, airflow can decline sharply as passages close. Treating fan airflow as unchanged can materially overpredict the usable refrigeration period.
The boundary conditions need to reflect the actual application. Specify entering-air conditions as a time profile when door openings, product loading, compressor cycling, or ambient variations are material. For a unit cooler, infiltration events may impose short intervals of high moisture load that dominate frost accumulation. A steady psychrometric condition can be appropriate for screening, but it should not be mistaken for a full operating forecast.
A physical framework for frosting simulation
A practical engineering model divides the coil into small control volumes along both the air and refrigerant paths. Within each control volume, the calculation evaluates local air temperature, humidity ratio, refrigerant state, tube-wall temperature, fin temperature, and frost thickness. The model advances through time as frost mass is deposited.
The local frost mass rate is driven by vapor transport from the air stream to the cold surface. In simplified form, the deposition rate depends on the local mass-transfer coefficient and the difference between bulk-air vapor concentration and vapor concentration at the frost surface. The surface condition is tied to frost-surface temperature, which is itself determined by the coupled heat balance through the frost layer, fin, tube wall, and refrigerant.
At each time step, deposited mass increases local frost thickness according to the assumed or calculated frost density. That new thickness changes thermal resistance and the open-flow geometry between fins. The air-side heat transfer coefficient and pressure drop must then be recalculated, followed by the fan operating point and refrigerant-side solution. This iterative process is essential because the variables do not change independently.
For DX coils, the refrigerant calculation should account for pressure drop, phase change, superheat development, and circuit distribution. A frost model coupled only to a uniform evaporating temperature can be useful for early feasibility work, but it can obscure the localized conditions that determine frost onset. Parallel circuits with unequal loading may show substantially different frost thicknesses even when the average suction pressure appears normal.
Represent frost structure with appropriate rigor
The level of frost-property detail should match the decision being made. For comparative studies of fin spacing or circuit arrangement, a calibrated effective-density and conductivity correlation may be adequate. For defrost optimization, capacity guarantees, or equipment intended for demanding low-temperature service, the model should allow frost properties to vary with temperature, deposition rate, and time.
The trade-off is computational cost and parameter uncertainty. A highly detailed frost-density model does not improve a prediction if entering-air moisture load, fan curve, or air maldistribution is poorly defined. Engineering-grade analysis should prioritize the parameters with the greatest influence on the decision, then quantify sensitivity around uncertain inputs.
Particular attention is warranted near the fin leading edge. Frost can bridge narrow fin channels early in the exposure period, producing a disproportionate pressure-drop increase before average frost thickness appears severe. Conversely, a model based only on average coil loading may miss a localized blockage pattern caused by uneven face velocity or a colder circuit region.
Defrost should be part of the operating model
Defrost is not merely the endpoint of a frosting calculation. It affects the next frost cycle through retained water, coil thermal mass, fan restart timing, drainage performance, and recovery load. A useful model evaluates the full sequence: frost growth, defrost initiation, heat addition or hot-gas flow, melt and drainage, termination, and post-defrost pull-down.
Defrost initiation criteria should reflect the controlled variable in the actual equipment. Common choices include elapsed time, coil pressure drop, airflow, temperature differential, capacity loss, or a sensor-derived frost indicator. Time-based defrost is straightforward to model, but it can produce unnecessary energy use under low-moisture conditions and inadequate protection during high-infiltration periods. Demand-based logic can improve performance, provided the sensing strategy remains reliable as coil conditions vary.
Termination criteria also matter. Ending electric defrost on a single temperature measurement can leave residual ice in colder regions of a large coil. Continuing too long increases energy consumption and can impose unnecessary product or space-temperature excursions. The simulation should therefore report both defrost energy and post-defrost recovery, not just the interval between events.
How to validate a frosting model
Validation should compare transient behavior, not only clean-coil capacity. Measured coil pressure drop, airflow or fan power, suction pressure, air-off temperature, and defrost interval provide a stronger basis for evaluating the model. Where possible, record entering-air humidity and operational events such as door openings, fan cycling, and defrost commands.
A good validation sequence starts with clean-coil thermal and pressure-drop performance. Next, verify the predicted trend in airflow and pressure drop during frost accumulation. Then compare the predicted defrost trigger and recovery response. If the clean coil does not match test data, adding frost correlations will not correct the underlying geometry, airflow, or refrigerant-distribution error.
Sensitivity analysis is equally valuable. Vary entering humidity, face velocity distribution, frost density, fan curve tolerance, and refrigerant saturation temperature across credible bounds. The result should identify whether a design is resilient or whether a small change in operating conditions creates an unacceptable reduction in run time or capacity.
Using frosting results in coil design decisions
The most useful output is rarely a single frost thickness. Design teams need time-resolved capacity, airflow, pressure drop, fan power, refrigerant conditions, and defrost energy. These outputs reveal whether a larger face area, wider fin pitch, revised circuitry, different fan selection, or altered defrost strategy offers the best system-level result.
Wider fin spacing can extend operating time before blockage, but it may reduce clean-coil surface area and require a larger coil envelope. Higher face velocity can reduce cabinet size, yet it often accelerates pressure-drop growth and increases fan energy. Lower evaporating temperature can satisfy load at a given condition while increasing frost propensity. There is no universal optimum; the correct choice depends on the required duty cycle, moisture exposure, space constraints, and energy objective.
Professional HVAC&R software such as ExCoil is most valuable when it connects detailed coil geometry and refrigerant behavior to these changing air-side conditions. The goal is not to produce a visually convincing frost profile. It is to make defensible decisions before prototype testing reveals a limitation that the clean-coil rating could never show.
A well-constructed frosting simulation turns defrost interval, airflow degradation, and transient capacity from assumptions into design variables. Use it early enough that fin geometry, circuit layout, fan selection, and control logic can still be changed at low cost.