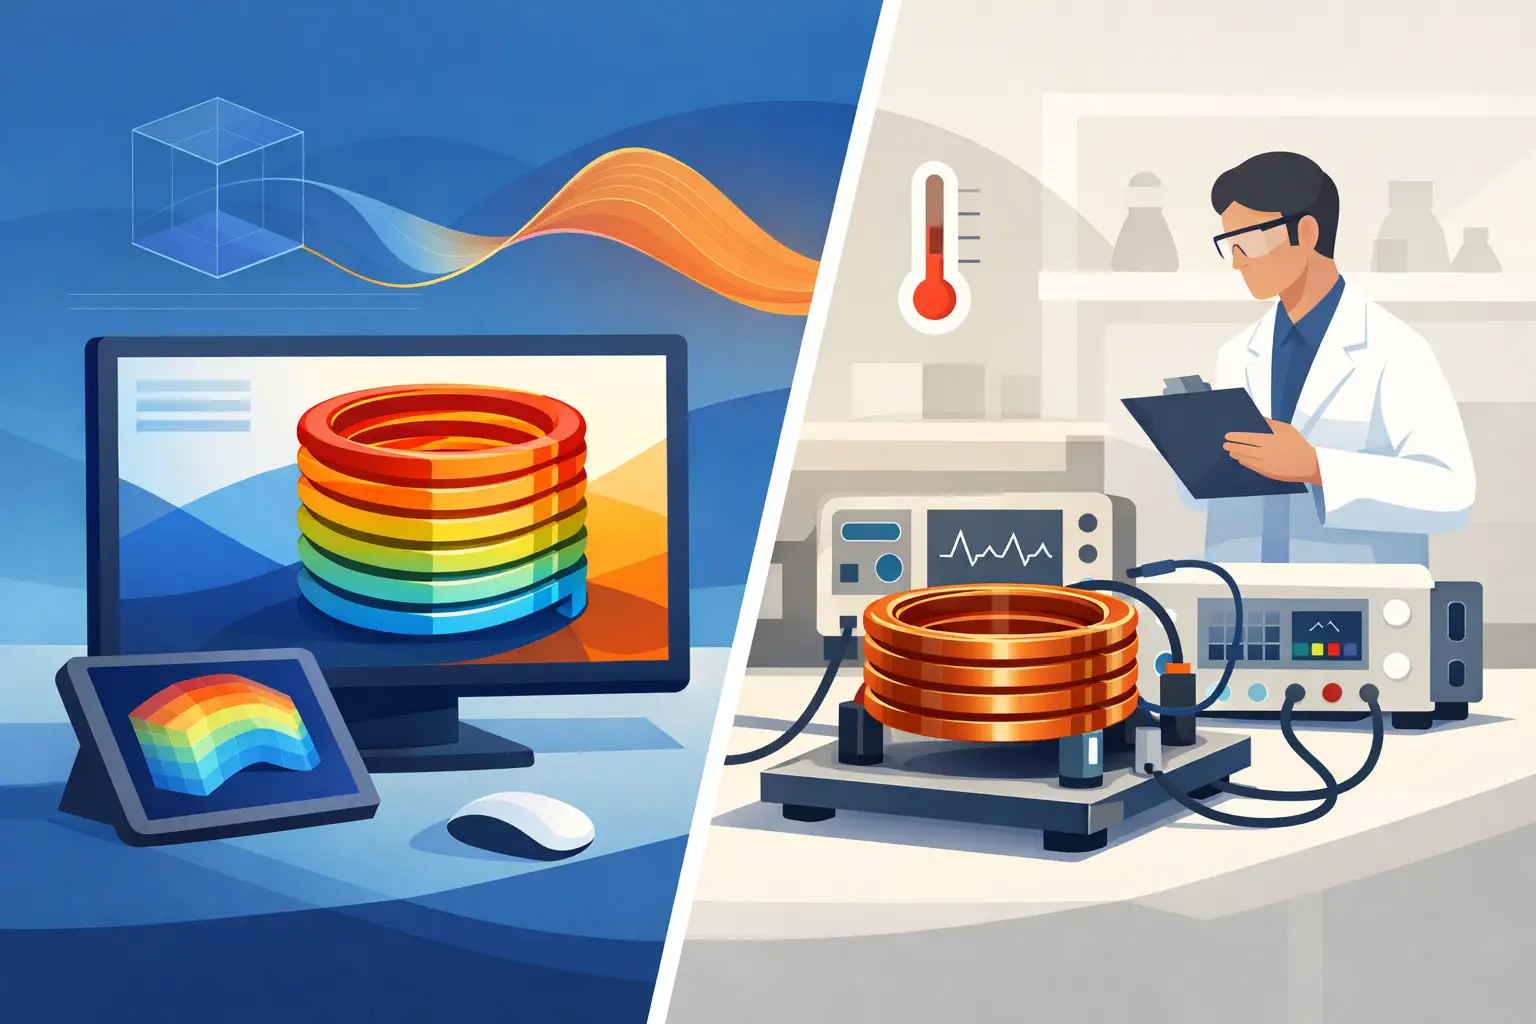
A prototype DX coil can meet capacity in a controlled calorimeter and still create a costly problem in production. The cause may be a circuiting detail, nonuniform face velocity, refrigerant distribution behavior, or a test condition that does not represent the final unit. Thermal simulation versus lab testing is therefore not a choice between a theoretical method and a real-world method. For evaporator and condenser development, it is a decision about when to generate insight, when to establish evidence, and how to correlate the two.
For HVAC&R engineering teams, the most effective workflow uses both methods for the work each does best. Engineering-grade thermal analysis provides rapid visibility into design sensitivity before hardware exists. Laboratory testing establishes measured performance, exposes physical effects not represented by the model, and supplies the data required to improve confidence in subsequent calculations.
Thermal Simulation Versus Lab Testing: Different Evidence
Thermal simulation predicts coil behavior from a defined description of the heat exchanger and its operating conditions. Depending on the model scope, inputs can include tube and fin geometry, circuitry, tube count, circuit arrangement, airside conditions, refrigerant selection, saturation conditions, superheat or subcooling targets, airflow, and pressure-drop assumptions. The output is not merely a capacity estimate. A suitable coil model can show how capacity, airside pressure drop, refrigerant pressure drop, leaving-air condition, surface temperature, and refrigerant state change across the coil.
This makes simulation especially valuable during early design. An engineer can compare circuit arrangements, fin spacing, face area, tube geometry, and operating points without fabricating every candidate. It also supports sensitivity analysis. If a condenser is unusually sensitive to entering-air temperature or a low-temperature evaporator is strongly affected by airflow reduction, that information can shape the design before a formal test program begins.
Laboratory testing answers a different question: what did this physical coil do under these measured conditions? A properly controlled calorimeter or psychrometric test setup captures the combined effect of actual manufacturing details, distributor behavior, contact resistance, airflow nonuniformity, instrumentation, controls, and installation configuration. Test results are the basis for rating, qualification, customer requirements, and confidence that a production-representative design performs as intended.
Neither source of evidence is automatically superior in every situation. A lab result is only as representative as the specimen, test setup, instrumentation accuracy, and selected conditions. A simulation is only as credible as its physical correlations, inputs, boundary conditions, and applicability to the coil being analyzed.
Where Thermal Simulation Provides the Highest Value
Simulation has a substantial advantage when the engineering question involves many possible designs or conditions. Building and testing a single prototype can take weeks. Evaluating a matrix of tube circuits, fin patterns, airflow rates, condensing temperatures, and refrigerant conditions through physical testing alone can consume a significant development budget.
For a DX evaporator, consider circuiting selection. A model can identify whether a proposed arrangement produces excessive refrigerant pressure drop, insufficient exit superheat, undesirable surface-temperature distribution, or poor utilization of available airside temperature difference. The engineer can then direct prototype effort toward a smaller set of credible options rather than testing every layout that can be drawn.
For condensers, simulation is useful for examining performance across high ambient conditions, changing airflow, and different refrigerant mass flow rates. It can indicate where a design approaches a pressure-drop or fan-power constraint and whether additional surface area delivers useful capacity or only marginal improvement. This is particularly relevant when system-level performance depends on condensing temperature as much as nominal heat rejection.
The quality of the inputs determines whether this insight is actionable. Coil geometry must reflect the intended hardware. Airflow must be defined in terms meaningful to the equipment, including face velocity and anticipated maldistribution where applicable. Refrigerant conditions must match the system state being evaluated, rather than relying on a generic rating point. Specialized professional HVAC&R software such as ExCoil is intended for this type of component-level thermal analysis, where design variables and operating assumptions need to be visible and technically defensible.
What the Laboratory Can Reveal That a Model May Not
A thermal model cannot correct an unknown physical condition. Laboratory testing is indispensable when design performance depends on effects that are poorly characterized, difficult to measure before fabrication, or outside the model's validated range.
Refrigerant distribution is a common example. A coil calculation may assume the flow entering each circuit is distributed according to the design intent. The actual distributor, nozzle selection, feeder geometry, orientation, pressure drop, and operating load can produce a different result. If circuits are unequally fed, part of the evaporator surface may operate at a markedly different refrigerant state than predicted, affecting capacity, superheat, and return-gas behavior.
Airside behavior can create similar discrepancies. Fan discharge patterns, bypass paths, cabinet restrictions, coil mounting, and frost accumulation can all change local air velocity. A coil tested in an idealized air tunnel may not respond the same way once installed in a packaged unit. For applications with low allowable airside pressure drop, even small construction or assembly differences can matter.
Testing is also needed to establish physical durability and repeatability. Thermal capacity calculations do not verify leakage, vibration resistance, header integrity, drainage, condensate carryover, oil return, or manufacturing consistency. These are not shortcomings of simulation. They are separate engineering questions that require a physical article and an appropriate test method.
Correlation Is More Valuable Than Either Method Alone
The strongest development process treats lab testing as an input to model confidence, not as a final pass-fail event performed after design decisions are fixed. When calculated and measured results differ, the goal is not to force agreement by applying an arbitrary correction factor. The goal is to identify the cause of the difference.
Start by confirming that the simulated and tested cases are genuinely equivalent. This requires more discipline than it appears. Compare refrigerant type and composition, entering-air dry-bulb and humidity, air volume, barometric pressure where relevant, saturation temperatures or pressures, superheat, subcooling, and the location of measured temperatures and pressures. Confirm the tested coil matches the geometry and circuitry represented in the model, including fin density, tube dimensions, distributor components, and number of active circuits.
Next, separate measurement uncertainty from model discrepancy. Capacity calculated from an airside enthalpy difference depends on airflow measurement, temperature measurement, humidity measurement, and stability. Refrigerant-side calculations have their own sensitivity to mass flow, property data, pressure location, and heat loss. A 3 percent difference may be meaningful in one test program and within expected uncertainty in another.
Once the test condition is credible, examine the pattern rather than one isolated result. If a model agrees at nominal airflow but overpredicts at low airflow, the issue may be related to airside heat transfer, bypass, or flow distribution. If the difference grows at high load, refrigerant-side pressure drop or distribution may warrant investigation. A correlation based on multiple operating points is more useful than a correction tuned to one rating condition.
Selecting the Right Method by Development Stage
The appropriate balance changes over the life of the coil. Early concepts benefit from broad simulation because the design space is still open. During detailed design, simulation can narrow choices and identify operating limits. Prototype testing then verifies the preferred design and provides data for correlation. Preproduction testing confirms that manufacturing-representative hardware retains the expected performance.
Use simulation first when the question is comparative: Which circuit arrangement is likely to provide the best balance of capacity and pressure drop? How much performance is lost at reduced airflow? Does a change in fin spacing improve the intended operating envelope? These questions require fast iteration and consistent assumptions.
Use lab testing first when the question is physical or contractual: Does the unit meet a specified rating? Does the distributor feed the coil acceptably? Does the cabinet create airflow bypass? Will the product satisfy a customer qualification procedure? In these cases, measured results are the required evidence.
For major design changes, avoid replacing one method with the other. A laboratory test may demonstrate nominal capacity while missing off-design weaknesses that simulation would reveal. A detailed model may predict an attractive result while missing a prototype-specific distribution issue. The cost of using both intelligently is generally lower than the cost of discovering a performance shortfall after tooling, certification, or release.
Building a Defensible Thermal Analysis Workflow
A practical workflow begins with a clear engineering question and a controlled input set. Define the performance metric first: net capacity, sensible capacity, leaving-air condition, refrigerant pressure drop, fan-energy impact, or a system-level condensing or evaporating temperature target. Then establish the operating envelope rather than relying solely on one nominal point.
Maintain traceability between the coil model and test article. Record geometry revisions, circuitry drawings, distributor details, refrigerant charge approach, test instrumentation, and data-reduction methods. When a result changes, this record prevents teams from debating whether the cause was the design, the test condition, or the analysis setup.
Most importantly, treat disagreement as useful information. A measured deviation can expose a design constraint that deserves attention. A simulated trend can reveal that a passing prototype has little margin at another operating point. The objective is not to declare a winner in thermal simulation versus lab testing. It is to build a coil design whose predicted behavior, measured performance, and production intent remain aligned when operating conditions become less forgiving.